Direct Answer: Run a Factory Acceptance Test as a witnessed comparison between released purchase requirements and objective evidence from the equipment that will ship. It is not a factory tour or a generic tick sheet.
Freeze the acceptance basis before the test date
The FAT can only be as clear as its reference documents. Before travel, the buyer and supplier should agree which purchase specification, approved drawings, data sheets, interface schedules, material requirements, software revision and deviation approvals form the baseline. Each document needs an identifiable revision. If the factory is building from a different revision, stop and reconcile the baseline before testing.
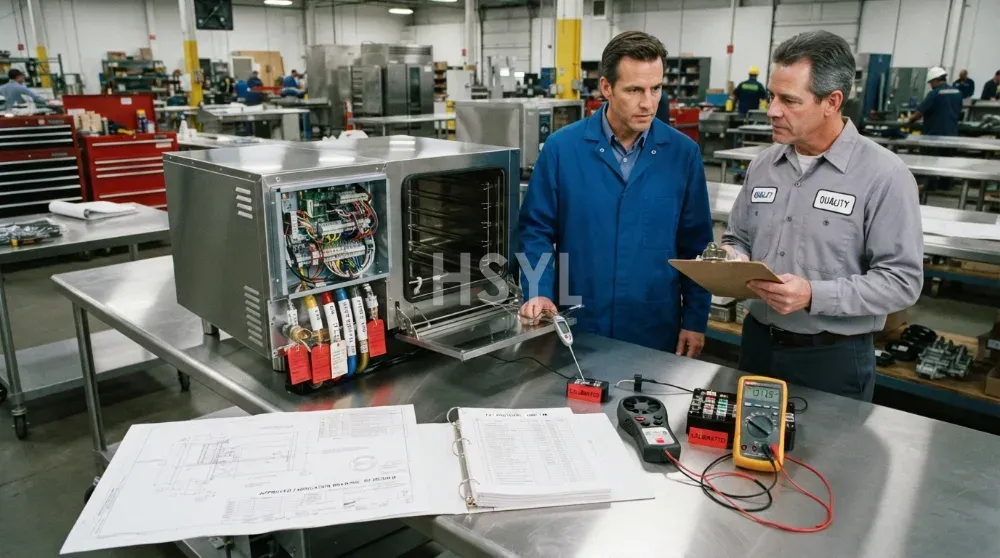
Define witness, review and hold points. State who can accept results, who can classify deviations and who can authorize release. Separate factory checks from tests that require site utilities, connected systems or local authority presence. The quality-control page may help structure supplier evidence, but project-specific requirements remain controlling.
| Acceptance source | Typical content | FAT use | Control question |
|---|---|---|---|
| Purchase specification | Scope, duty, materials, features and deliverables | Primary acceptance basis | Is every requirement traceable to a check or document? |
| Approved drawings | Dimensions, connections, access and construction details | As-built comparison | Is the witnessed unit built to the released revision? |
| Interface schedule | Electrical, water, drain, gas, steam, exhaust and controls | Connection verification | Do labels and physical locations match the site design? |
| Approved deviations | Buyer-authorized departures from the original requirement | Revised pass criterion | Is approval explicit and attached to the affected requirement? |
Complete the document review before touching the machine
Start with the document register. Review general arrangement and fabrication drawings, electrical diagrams, component schedules, operating and maintenance manuals, spare-parts recommendations, calibration records, inspection certificates required by contract and packing instructions. “Available after shipment” is not a pass when the purchase order requires the document at FAT.
Check consistency across documents. Rated data on the nameplate, data sheet, wiring diagram and utility schedule should refer to the same configuration. Material evidence must map to the parts covered by the specification; a certificate without traceability to the witnessed assembly proves little. For destination-market planning, use the destination-market requirements page as a coordination prompt, not as proof of product compliance.
Inspect identity, workmanship and cleanability
Confirm equipment identity, serial or project marking, model designation and major bought-out components against the approved schedule. Then inspect accessible surfaces, welds, joints, edges, panels, doors, fasteners, seals, drains, castors, guards and labels. Record observations with a location reference and image; adjectives such as “good finish” are not auditable evidence.
Cleanability checks should follow the intended sanitation method. Look for inaccessible soil traps, unsealed penetrations, retained liquid, mixed-metal contact, difficult-to-remove parts and fasteners exposed in food zones. Verify that removable parts can be removed and replaced by the intended operator using the agreed tools. Where food-contact material declarations are required, link them to the food-contact materials requirements and the project contract.
Run functions through normal, boundary and fault states
Operate every buyer-required function rather than merely energizing the unit. Follow the operating sequence from startup through loading, control, discharge, cleaning mode and shutdown. Test selectors, indicators, alarms, doors, latches, tilt or lift motions, pumps, fans, valves and programmed steps applicable to the supplied configuration.
Then challenge boundary and fault behavior agreed in the protocol. Examples include opening an interlocked guard, interrupting a permissive, removing a sensor signal through an approved simulation, or attempting an invalid command. Never improvise a hazardous fault. The method, safe state and expected reset behavior must be reviewed before execution.
| Test family | Example method | Evidence captured | Pass basis |
|---|---|---|---|
| Normal sequence | Run the approved operating cycle with representative controls | Step record, screen states and observations | Released functional description |
| Interlock | Apply the agreed interlock condition using a safe method | Output state, alarm and reset behavior | Cause-and-effect requirement |
| Mechanical motion | Exercise doors, tilts, lifts, castors and restraints under agreed condition | Travel, stability, interference and operator access | Approved drawing and risk controls |
| Cleaning access | Demonstrate disassembly, drainage and reassembly | Access record and retained-liquid observation | Sanitation procedure and design requirement |
Verify safety against the applicable design basis
Safety acceptance is market- and product-specific. The protocol should identify the governing electrical, gas, pressure, machinery, fire and hygiene requirements before the unit is built. FAT personnel must use approved procedures and competent test specialists. Do not copy resistance values, test voltages, leakage limits or protection ratings from another project.
At minimum, review protective devices, emergency actions where specified, guards, hot-surface warnings, sharp-edge control, stability, bonding arrangements, over-temperature protection and isolation points relevant to the equipment. Verify test-instrument identification and calibration status. The electrical standards page can organize questions, while the buyer’s named standard and destination authority define acceptance.
Check every site interface and control handoff
Compare connection type, location, orientation, access and labels with the coordinated site drawing. Include electrical supply, earthing or bonding provisions, water quality and pressure requirements, drains, gas, steam and condensate, exhaust, data, remote enable and alarm contacts as applicable. A correct connector in the wrong location can still force a site modification.
Where factory utilities differ from the final site, record the limitation and its effect on test validity. Identify open items for Site Acceptance Testing rather than treating them as passed. Photograph connection panels with a scale reference, and confirm that shipped loose items, mating parts and installation instructions are included in the packing list.
Prove performance with a representative load and an agreed method
Performance testing needs a written method: product or simulant, initial condition, load pattern, ambient conditions, instrument locations, stabilization rule, sampling interval and acceptance criterion. The most useful method resembles the buyer’s duty while remaining repeatable. A no-load display reading does not prove loaded recovery, temperature distribution, washing result or production behavior.
Record raw data, not only a pass statement. If the result depends on a recipe or control setting, preserve that revision. For cooking, chilling, washing or holding equipment, define what will be measured and who owns food-safety interpretation. Never state an HSYL capacity, temperature, efficiency or cycle time unless the exact model and witnessed method support it.
Control software, labels, spares and shipment configuration
Record controller, HMI and recipe revisions when software is part of the supply. Confirm language, units, access levels, backup procedure, alarm text and restoration method against the contract. Save approved parameter files through the agreed transfer process. A screenshot alone may not be sufficient to restore a controller after replacement.
Check nameplates, hazard labels, cleaning labels and utility identification for language and destination requirements. Reconcile standard accessories, loose parts, special tools, consumables and agreed spares with the packing list. The spare-parts support page is a useful internal reference, but the project list must identify exact supplied items.
Close deviations through evidence, not optimistic wording
Every failed or incomplete check needs a unique record tied to the requirement, unit and location. State the observed condition, evidence, risk, containment, owner and proposed disposition. Distinguish correction of the observed defect from corrective action addressing its cause where the quality process requires both.
The ISO and IAF auditing guidance on reviewing and closing nonconformities emphasizes correction, cause analysis and corrective action. Apply that discipline proportionately. A photograph of rework may close a cosmetic item; a failed protection function normally requires retest evidence and review of affected units.
| Deviation field | Required entry | Why it matters |
|---|---|---|
| Requirement reference | Specification, drawing or protocol clause and revision | Defines what was not met |
| Objective evidence | Observation, data, image and equipment identity | Makes the record reproducible |
| Disposition | Repair, replace, accept by concession or retest as authorized | Prevents informal closure |
| Closure evidence | Reinspection, retest, revised document and approval | Shows the requirement is now satisfied or formally changed |
Release for packing only after the dossier is coherent
The final review should reconcile the checklist, raw test data, calibration status, photographs, deviations, approved concessions, software backup, manuals, certificates and packing list. Mark unresolved site-only checks explicitly. The release signature should state what is accepted, what remains open and whether packing may proceed.
Use the evidence center and installation and commissioning guidance to keep the handoff connected. FAT approval does not replace receiving inspection, installation checks or site acceptance; it reduces avoidable uncertainty before the equipment leaves the factory.