Direct Answer / Key Takeaway: Industrial specification review of Heavy-Duty Gas Range NSF/ANSI splash zone hygiene and cleanability. Review OEM engineering specs and MEP standards from HSYL.
Optimizing commercial kitchen reliability requires rigorous alignment between equipment performance and facility operational demands. This document provides an exhaustive technical breakdown of Standard Duty Heavy-Duty Gas Range configurations across nsf/ansi sanitation certification, detailing empirical sizing models, MEP rough-ins, and preventive maintenance protocols.
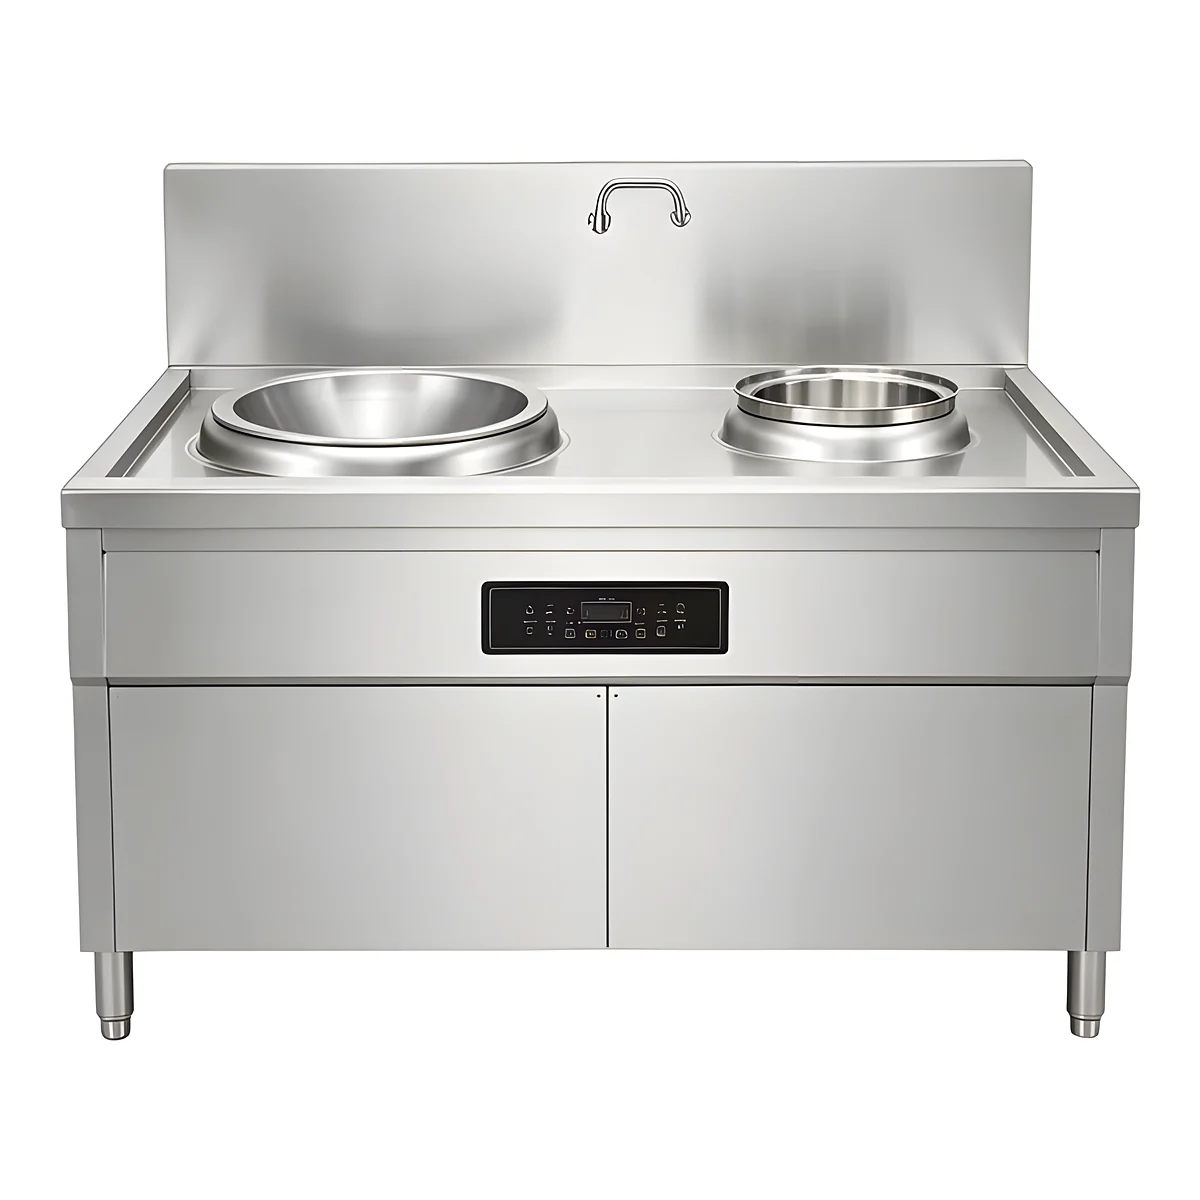
1. Commercial Brigade Deployment & Kitchen Line Harmony: NSF/ANSI Sanitation Certification
NSF/ANSI Standard 2/4/7 Sanitary Geometry & Cleanability Criteria:
Commercial foodservice equipment operating in regulated North American and European markets must comply with rigorous public health sanitation standards established by NSF/ANSI. The standard delineates equipment into three distinct hygiene zones: Food Zone (direct food contact surfaces), Splash Zone (surfaces subject to splashing, spillage, and soiled droplet contact during routine operation), and Non-Food Zone. Food Zone and Splash Zone engineering prohibits external screw threads, exposed piano hinges, rolled sheet metal lips, and 90-degree internal square corners that harbor bacterial biofilms (e.g., Listeria monocytogenes and Salmonella). All internal tank and cavity corners must feature continuous coved radii measuring at least 6.4 mm (1/4 inch), fully welded and ground to a smooth #4 sanitary polish (surface roughness Ra < 0.8 um / 32 micro-inches). Fasteners within splash zones must feature sanitary domed acorn nuts with enclosed threads; sliding doors and pan runners must be removable by hand without tools to facilitate daily washdown sanitization.
When sizing equipment for peak production hours, facility planners must reference verified heavy-duty commercial combi oven specifications to ensure capacity reserves remain aligned with scheduled shift turnover targets.
2. Physical Specification Matrix & Institutional Performance Tiers
To assist engineering procurement teams, the matrix below details metallurgical standards, utility ratings, and structural tolerance thresholds for commercial versus heavy-duty Standard Duty Heavy-Duty Gas Range configurations:
| Engineering Parameter | Standard Commercial Spec | Heavy-Duty Institutional Spec | Engineering Variance Threshold |
|---|---|---|---|
| Material Construction | AISI 304 (1.2 mm), 380V-415V 3N~ 50/60Hz (12-24 kW), DN15 soft water, IPX4 | AISI 304/316L (1.5-2.0 mm), 380V-415V 3N~ (28-48 kW), integrated boiler steam, IPX5 | +-0.05 mm chassis gauge, thermal uniformity +-2.0 deg C across all shelf tiers |
| Primary Engineering Feature | Chamber Construction: Double-glazed Low-E tempered glass door with multi-point halogen illumination | Reinforced industrial assembly with seamless continuous laser welds | Zero structural deflection under maximum rated loading |
| Operational Subsystem | Steam Generation Duty: Hybrid boiler injection with dynamic variable-frequency fan reversing | High-efficiency heavy-duty components with dynamic feedback telemetry | Energy efficiency index within top 10% commercial benchmark |
| Sanitary & Safety Rating | Drainage & Effluent: DN40 indirect drain with integrated steam condensing temper quench | IPX5 washdown protection with NSF/ANSI cleanability rating | Hermetic perimeter sealing preventing microbial colonization |
3. Thermodynamics, Fluid Dynamics & Operating Mechanics
Thermodynamic Forced Convection & Enthalpy Control: Commercial combi and convection ovens utilize high-efficiency bidirectional radial blowers to circulate heated air across all pan levels. Heat transfer occurs through forced convective heat flux, compressing thermal boundary layers on food surfaces. When steam injection is engaged, the latent heat of condensation (2,260 kJ/kg) deposits instantaneous thermal energy onto the product, accelerating core cooking rates while maintaining food moisture content. Precision motor inverters dynamically adjust fan revolutions from 300 to 1,500 RPM, preventing delicate pastry dehydration while providing high-velocity shearing air for roasting.
In institutional catering environments, equipment longevity is heavily governed by surface passivation and corrosion resistance. Units fabricated from high-grade austenitic stainless steel must maintain an uncompromised chromium oxide passivated boundary layer. Regular chemical cleaning with non-abrasive detergents prevents pitting attack from chlorinated sanitizers and atmospheric chlorides.
Understanding these thermodynamic and mechanical principles allows consulting engineers to optimize cycle times, reduce utility peak draw, and eliminate premature component fatigue.
4. Rigorous Capacity Derivation & Meal Turnover Equations: Pan Tier Sizing Formula
Determining optimal unit capacity demands empirical engineering formulations rather than rule-of-thumb approximations. Planners apply the following equation to size continuous throughput:
Required Pan Tiers (GN 1/1) = [Peak Banquet Meals * Portion Mass (0.35 kg)] / [Average Pan Yield (4.5 kg) * Batch Turnover Rate (1.2)]
For a 350-cover dining wave requiring batch roasting completed within 75 minutes: Net Mass = 122.5 kg; Total required GN 1/1 pan slots = 23 tiers (specifying a 20-tier roll-in or twin 10-tier combi stack).
Practical sizing engineering requires accounting for the hidden ware factor. Beyond customer dining covers, back-of-house food preparation items (hotel pans, sheet trays, mixing bowls, and prep utensils) contribute an additional 15% to 20% to total kitchen processing loads. Furthermore, thermal transfer times for bulk foods follow the transient conduction square-law relationship (t is proportional to x^2), meaning doubling product depth from 50 mm to 100 mm in pans roughly quadruples core pull-down or heating times. Sizing calculations must incorporate these empirical variables to ensure uninterrupted kitchen workflow.
Employing this sizing method protects the kitchen from meal bottlenecks, prevents premature thermal and mechanical failure, and guarantees compliance with HACCP time-temperature critical control points (CCP).
5. Facility Interface Engineering, Utility Rough-Ins & Clearances
Mechanical, electrical, and plumbing infrastructure must be properly prepared prior to equipment delivery. The following engineering specifications govern site hookups for Standard Duty Heavy-Duty Gas Range:
- Power & Electrical Connection: Dedicated 3-phase 380V-415V circuit with Type C industrial breaker and local lockable isolator switch.
- Water Supply & Treatment: Filtered cold water via reverse osmosis (< 50 ppm TDS, hardness < 3 gpg, chloride < 25 ppm) to prevent boiler scaling.
- Wastewater & Drainage Air Gap: Discharges must connect to temperature-resistant indirect waste lines with an unobstructed physical air gap, conforming to FDA Food Code Chapter 4 backflow mandates.
- Ventilation, Clearances & Environment: Exhaust hood overhang of min 300 mm past equipment footprint; min 150 mm rear air gap for convection fan intake; Type I canopy with UL 710 grease filters.
Critical Field Installation Redlines & Contractor Pitfalls: During jobsite rough-ins, engineering teams must enforce the following compliance boundaries to prevent premature equipment failure and voided warranties:
- Drain Ingress Under Footprint: Never rough-in an open floor sink directly beneath the oven base; rising steam and chemical vapors will penetrate bottom louvers, causing catastrophic motherboard corrosion.
- Control Side Clearance: Maintain minimum 450 mm (18 inches) unobstructed clearance on the control side; restricted space blocks technician access and incurs costly service surcharges.
- Boiler Raw Water Scaling: Do not connect steam boiler feeds to untreated raw water; scale accumulation on heating immersion elements will void manufacturer warranty within 90 days.
6. Quality Verification Audits, FAT Dossiers & Certifications
Factory acceptance protocols establish that equipment performance conforms to engineering shop drawings and international safety standards. Auditing teams verify factory acceptance testing and compliance verification across the following tests:
- Dielectric High-Voltage Insulation: Verified at 1500V AC for 60s between heating elements and grounded chassis with leakage current under 3.0 mA.
- Thermal Hold Stability Test: 120-minute continuous dry-heat test at 250 deg C; temperature variation across 20 pan positions strictly within +-2.0 deg C.
- Steam Generator Scaling Delta-P Audit: Dynamic steam injection pressure tested at 1.5 bar with optical conductivity probe verification.
- Double-Glazed Door Hermetic Clamp Test: 360-degree perimeter paper clamp pull test ensuring zero thermal air leakage around silicone door gaskets.
To satisfy commercial health department and third-party food safety audits, modern commercial appliances incorporate automated HACCP data logging. The onboard microcomputer logs real-time time-temperature decay profiles, cycle durations, and sanitizing rinse parameters with cryptographic timestamps. Facilities personnel can export encrypted audit logs via USB or Modbus/Ethernet IoT interfaces, providing verifiable compliance dossiers to satisfy municipal health inspectors during unannounced regulatory audits.
7. Diagnostic Logic, Failure Modes & Root Cause Troubleshooting
Microprocessor control boards continuously monitor operational health. When anomalous readings occur, technicians should apply the corrective protocols detailed in this diagnostic matrix:
| Fault Code | Root Cause Diagnostic | Corrective Maintenance Procedure |
|---|---|---|
| E08 | Steam Boiler Descaling Alert | Pressure drop across boiler heat exchanger exceeds 0.4 bar; trigger auto-decalcification cycle. |
| E14 | Multi-Point Core Thermal Probe Drift | Temperature differential between internal sensors exceeds 3.0 deg C; calibrate in ice bath. |
| E21 | Convection Fan Motor VFD Fault | Inverter overcurrent or tachometer pulse loss; verify motor windings and capacitor banks. |
8. Preventive Service Schedules & Long-Term Asset Protection
Planned maintenance protocols reduce catastrophic component failures and stabilize utility efficiency. Maintenance personnel must execute inspections per the following intervals:
| Maintenance Interval | Inspection Scope & Component Target | Acceptable Operating Standard |
|---|---|---|
| Daily Shift End | Chamber washdown, door seal wipe-down, drain strainer basket clear | Zero food residue, clear gravity drainage, supple silicone gasket |
| Monthly Maintenance | Water filter cartridge delta-P, chemical rinse tubes, hinge torque | Filter differential < 0.5 bar, no peristaltic hose cracking, smooth door latching |
| Quarterly Service | Heating element scale accumulation, electrical terminal torque, ground bond | Scale thickness < 0.2 mm, terminal torque to 2.5 N.m, ground resistance < 0.1 Ohm |
| Annual Overhaul | Full thermal probe calibration, solenoid valve replacement, contactor wear | Thermocouple drift within +-1.0 deg C, zero valve weeping, contact pitting < 15% |
All mechanical maintenance interventions must utilize NSF H1 certified food-grade synthetic lubricants on drive bearings and moving pivot hinges. Electrical connections, magnetic contactors, and grounding continuity must be re-torqued and tested annually using calibrated digital multimeters to prevent thermal resistance hot spots.
Recommended First-Year Commissioning & Preventative Spares Kit: For international projects and remote institutional complexes, maintaining an on-site critical spares inventory avoids catastrophic service interruptions:
| Part Description | Recommended Quantity | Engineering Maintenance Function |
|---|---|---|
| High-Temp Silicone Door Gasket | 2 Sets | Maintains hermetic chamber seal, preventing steam loss and door frame condensation. |
| Multi-Point Core Thermal Probe | 1 Piece | Calibrated insertion needle sensor ensuring HACCP core cooking temperature compliance. |
| Boiler Level Electrode Kit | 1 Set | Prevents dry-firing of boiler heating elements during high-volume steam cycles. |
| Solid-State Inverter Relay | 2 Pieces | Regulates bidirectional convection fan reversing and thermal contactor switching. |
9. Marine Container Packaging, Shock Telemetry & Export Standards
International export packaging must withstand cross-ocean container shipping, tropical humidity cycling, and intermodal transport vibration. Factory crating standards for Standard Duty Heavy-Duty Gas Range specify:
- Internal Rack Locking Brackets: Stainless transit lock bars clamping all interior trolley runners to eliminate transit rattle.
- Tempered Glass Face Cushioning: High-density polyethylene foam shield bonded over front door glass resisting point impacts.
- Hermetic VCI Barrier Enclosure: Multi-layer heat-sealed foil with 4 x 500g clay desiccant bags maintaining RH < 25% inside crate.
- ISPM-15 Certified Timber Crate: Heat-treated timber with external TiltWatch and 50G ShockWatch impact telemetry sensors.
For comprehensive wiring schematics, spare parts exploded diagrams, and maintenance schedules, consult the official technical documentation and installation manuals provided by HSYL engineering.