Direct Answer / Key Takeaway: Professional facility planning guide for Drop-in Heated Wells Buffet evaluating gas vs electric operating costs and recovery. Inspect engineering.
Selecting commercial kitchen appliances requires an evidence-based engineering assessment of operational loads, utility footprints, and lifecycle reliability. This specification guide analyzes Standard Duty Drop-in Heated Wells Buffet within the framework of gas vs electric operating cost & recovery comparison, providing consulting engineers and hospitality operators with rigorous technical benchmarks.
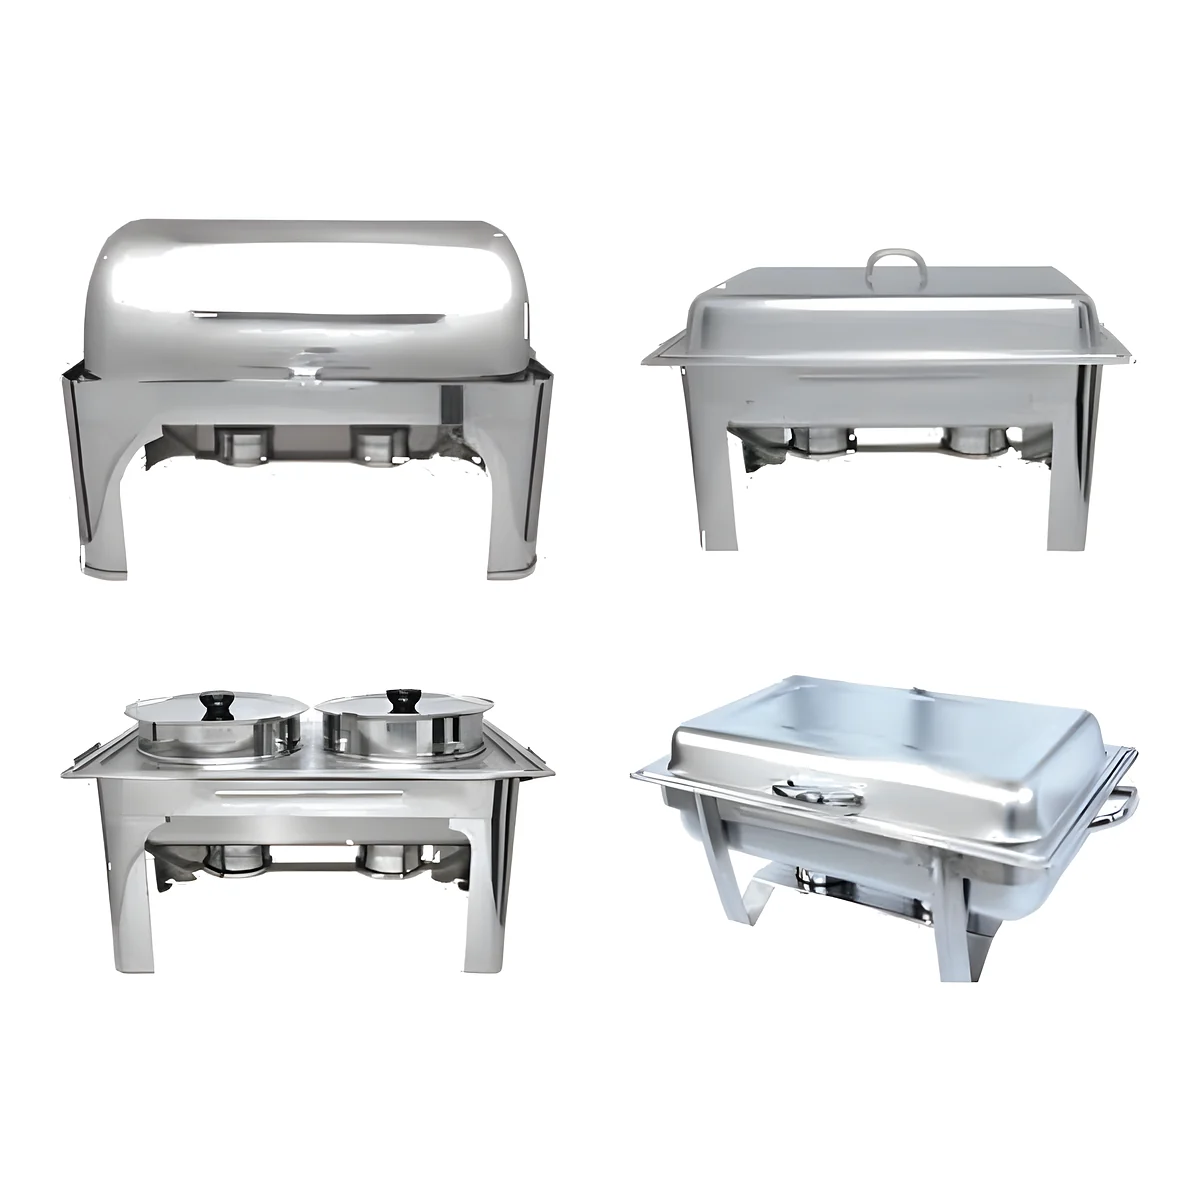
1. High-Volume Catering Scenarios & Station Architecture: Gas vs Electric Operating Cost & Recovery Comparison
Gas vs. Electric Energy Economics, Efficiency & Utility TCO Analysis:
Procurement evaluations between gas and electric commercial kitchen machinery require rigorous modeling of local utility rate tariffs against thermal conversion efficiency. Atmospheric natural gas burners deliver typical thermal transfer efficiencies of 40% to 50%, with the remaining sensible heat lost to exhaust flues and ambient air, whereas heavy-duty electric elements achieve 85% to 90% and commercial induction exceeds 90% efficiency. Consulting engineers calculate the operational breakeven threshold: Operating Cost/Hour = (Rated kW * Electricity Tariff $/kWh) versus ((Rated BTU/hr / 100,000) * Gas Tariff $/therm). While electric appliances deliver faster temperature recovery and reduce air conditioning loads, they demand expensive 3-phase high-amperage facility service upgrades. Conversely, gas appliances require investment in NFPA 96-compliant Type I commercial exhaust canopies, continuous dedicated make-up air (MUA) fan systems, and automated fire suppression interlocks, which significantly elevate upfront MEP capital expenditure (CAPEX).
When sizing equipment for peak production hours, facility planners must reference verified kitchen workflow optimization and ergonomic layout design to ensure capacity reserves remain aligned with scheduled shift turnover targets.
2. Engineering Specifications & Component Material Profiles
The baseline performance data below establishes critical dimensional profiles, energetic consumption limits, and material gauges for Standard Duty Drop-in Heated Wells Buffet deployed in institutional foodservice facilities:
| Engineering Parameter | Standard Commercial Spec | Heavy-Duty Institutional Spec | Engineering Variance Threshold |
|---|---|---|---|
| Material Construction | AISI 304 (1.0 mm), 220V-240V 1N~ (1.2-2.0 kW), forced convection air, dial thermostat 30-85 deg C | AISI 304 (1.2 mm), 220V-240V (2.5-3.5 kW), active humidity water reservoir, digital HACCP core log | Temperature differential between top and bottom pan tiers <= +-2.0 deg C |
| Primary Engineering Feature | Airflow Architecture: Ducted perimeter convection channel providing uniform non-drying thermal blanket | Reinforced industrial assembly with seamless continuous laser welds | Zero structural deflection under maximum rated loading |
| Operational Subsystem | Moisture Regulation: Ultrasonic or heated water reservoir maintaining 30% to 80% relative humidity | High-efficiency heavy-duty components with dynamic feedback telemetry | Energy efficiency index within top 10% commercial benchmark |
| Sanitary & Safety Rating | Chassis Ergonomics: Heavy-duty non-marking perimeter bumper and heavy-duty silicone door magnetic gaskets | IPX5 washdown protection with NSF/ANSI cleanability rating | Hermetic perimeter sealing preventing microbial colonization |
3. Core Operating Physics & Mechanical Subsystem Analysis
Gentle Conductive Thermal Enclosure & Humidity Management: Institutional food warming cabinets utilize low-density conductive heating cables wrapped around the external chamber perimeter, radiating gentle, radiant thermal warmth without forced convection fans. This radiant approach prevents dry, evaporative skinning of cooked proteins, sauces, and delicate starch preparations. Integrated digital humidity control maintains relative humidity (RH) between 60% and 85%, ensuring held food satisfies HACCP temperature minimums (> 60 deg C) over multi-hour holding intervals without flavor degradation or moisture loss.
In institutional catering environments, equipment longevity is heavily governed by surface passivation and corrosion resistance. Units fabricated from high-grade austenitic stainless steel must maintain an uncompromised chromium oxide passivated boundary layer. Regular chemical cleaning with non-abrasive detergents prevents pitting attack from chlorinated sanitizers and atmospheric chlorides.
Understanding these thermodynamic and mechanical principles allows consulting engineers to optimize cycle times, reduce utility peak draw, and eliminate premature component fatigue.
4. Production Yield Calculations & Mathematical Capacity Models: Holding Thermal Equilibrium Model
Kitchen throughput modeling relies on proven dimensional formulations to balance batch turnaround against meal wave surges. The calculation below defines nominal capacity requirements:
Heater Sizing (Watts) = [Surface Area (m2) * U-Factor (0.65 W/m2K) * Delta-T (55K)] + [Ventilation Latent Loss * Infiltration Factor (1.3)]
For a 22-tier mobile banquet cart maintaining 75 deg C in a 20 deg C room: Conduction loss = 4.8 m2 * 0.65 * 55 = 171.6W; Door opening infiltration loss = 950W; Total heating element size = 1,500W to ensure core temperatures stay strictly above 65 deg C.
Practical sizing engineering requires accounting for the hidden ware factor. Beyond customer dining covers, back-of-house food preparation items (hotel pans, sheet trays, mixing bowls, and prep utensils) contribute an additional 15% to 20% to total kitchen processing loads. Furthermore, thermal transfer times for bulk foods follow the transient conduction square-law relationship (t is proportional to x^2), meaning doubling product depth from 50 mm to 100 mm in pans roughly quadruples core pull-down or heating times. Sizing calculations must incorporate these empirical variables to ensure uninterrupted kitchen workflow.
Employing this sizing method protects the kitchen from meal bottlenecks, prevents premature thermal and mechanical failure, and guarantees compliance with HACCP time-temperature critical control points (CCP).
5. Utility Demands, MEP Rough-Ins & Architectural Coordination
Facility MEP coordination requires precise interface alignments to guarantee operating safety and code compliance. Verify the following site preparation standards for Standard Duty Drop-in Heated Wells Buffet:
- Power & Electrical Connection: Standard 220V-240V 10A/16A dedicated grounded outlet with retractable power cable reel.
- Water Supply & Treatment: Manual fill water pan or DN15 soft water inlet with overflow drain for active humidity models.
- Wastewater & Drainage Air Gap: Discharges must connect to temperature-resistant indirect waste lines with an unobstructed physical air gap, conforming to FDA Food Code Chapter 4 backflow mandates.
- Ventilation, Clearances & Environment: Level floor positioning with locking front casters; perimeter rubber bumpers protecting wall finishes during banquet cart transit.
Critical Field Installation Redlines & Contractor Pitfalls: During jobsite rough-ins, engineering teams must enforce the following compliance boundaries to prevent premature equipment failure and voided warranties:
- Holding vs Reheating: Never use warming cabinets to reheat cold food from refrigerated state; warmers maintain HACCP temperatures (> 60 deg C) but lack thermal flux to pass danger zones safely.
- Water Pan Scale Insulation: Descale bottom humidity water pans bi-weekly; mineral scale acts as thermal insulation, tripping high-limit safety thermostats prematurely.
- Door Gasket Seal Integrity: Check perimeter magnetic gaskets monthly; a warped gasket causes hot air convection leaks that dry out stored meats and sauces.
6. Manufacturing Standards, FAT Compliance & Safety Dossiers
Rigorous factory acceptance testing (FAT) guarantees that Standard Duty Drop-in Heated Wells Buffet satisfies all mechanical, electrical, and sanitary benchmarks prior to marine container loading. Review factory acceptance testing and compliance verification against these criteria:
- Cabinet Thermal Uniformity Audit: 16 thermocouple probes placed across all pan tiers verifying hold temp +-1.5 deg C at 75 deg C.
- Passive Thermal Retention Test: Cabinet disconnected from power; internal temp drop measured <= 2.5 deg C/hour.
- Humidity Generation Chamber Test: Relative humidity brought to 70% RH and maintained for 60 minutes with zero condensation puddling.
- Mobility & Caster Roll Resistance Test: Fully loaded 200 kg cart pushed across threshold test verifying smooth caster swivel.
To satisfy commercial health department and third-party food safety audits, modern commercial appliances incorporate automated HACCP data logging. The onboard microcomputer logs real-time time-temperature decay profiles, cycle durations, and sanitizing rinse parameters with cryptographic timestamps. Facilities personnel can export encrypted audit logs via USB or Modbus/Ethernet IoT interfaces, providing verifiable compliance dossiers to satisfy municipal health inspectors during unannounced regulatory audits.
7. Field Fault Diagnostics & Corrective Maintenance Logic
Resolving field service disruptions requires systematic root-cause diagnostics. Technicians should consult the following error code matrix to troubleshoot Standard Duty Drop-in Heated Wells Buffet:
| Fault Code | Root Cause Diagnostic | Corrective Maintenance Procedure |
|---|---|---|
| E02 | Humidity Water Reservoir Dry-Fire Alarm | Water level float dropped below minimum threshold; heating element isolated until tank replenished. |
| E06 | Relative Humidity Capacitive Sensor Drift | Sensor reports out-of-range RH reading; clean protective PTFE sintered sensor filter cap. |
| E12 | Door Gasket Magnetic Seal Air Infiltration | Cabinet temp drop rate exceeds 2 deg C/min with heater active; replace compressed perimeter gasket. |
8. Preventive Maintenance Protocols & Lifecycle Management
Operational reliability over a 10-year design horizon demands routine mechanical and electrical verification. Execute the following preventive maintenance schedule for Standard Duty Drop-in Heated Wells Buffet:
| Maintenance Interval | Inspection Scope & Component Target | Acceptable Operating Standard |
|---|---|---|
| Daily Shift End | Empty and clean humidity water reservoir, wipe interior coved corners and seals | Chamber dry, water pan free of mineral sediment, magnetic door seal clean |
| Weekly Operational | Inspect caster swivel bearings, verify door latch positive catch tension | Casters rotate freely without thread binding, door latch engages with firm positive click |
| Monthly Descaling | Descale humidity heating elements using food-grade sulfamic acid solution | Heating elements restored to bright stainless finish with zero lime accumulation |
| Annual Servicing | Recalibrate digital thermostat thermocouple, inspect heating element insulation | Temperature readout within +-0.5 deg C of certified reference thermometer |
All mechanical maintenance interventions must utilize NSF H1 certified food-grade synthetic lubricants on drive bearings and moving pivot hinges. Electrical connections, magnetic contactors, and grounding continuity must be re-torqued and tested annually using calibrated digital multimeters to prevent thermal resistance hot spots.
Recommended First-Year Commissioning & Preventative Spares Kit: For international projects and remote institutional complexes, maintaining an on-site critical spares inventory avoids catastrophic service interruptions:
| Part Description | Recommended Quantity | Engineering Maintenance Function |
|---|---|---|
| Perimeter Conductive Cable Element | 1 Set | Low-watt-density radiant heating wrap providing gentle wrap-around thermal holding. |
| Analog/Digital Humidity Sensor | 1 Piece | Monitors RH% moisture levels to prevent surface dehydration of held meats and sauces. |
| Heavy-Duty Vulcanized Wheel Caster | 2 Pieces | High-rebound shock-absorbing caster with integrated non-slip foot brake. |
| Magnetic Paddle Door Latch Assembly | 1 Set | Positive slam-action latch keeping heavy cart doors closed during hallway transit. |
9. Industrial Export Packing, Moisture Barriers & Freight Protection
Marine transit across international shipping corridors requires engineered protective packaging to safeguard delicate electronic controls and stainless assemblies. Dispatch protocols for Standard Duty Drop-in Heated Wells Buffet include:
- Pan Slide Locking Channels: Removable stainless locking bar clamping all interior pan slides against transit movement.
- Perimeter Bumper Impact Wrap: Full perimeter non-marking rubber bumper wrapped in corrugated protective sleeve.
- Moisture-Barrier Crate Lining: Heavy-gauge heat-sealed polyethylene barrier bag enclosing complete cart.
- ISPM-15 Heat-Treated Crate: Sturdy timber box with internal wheel chocks preventing caster roll in container.
For comprehensive wiring schematics, spare parts exploded diagrams, and maintenance schedules, consult the official technical documentation and installation manuals provided by HSYL engineering.